Sample Evaluation Protocol for B2B Buyers of PU Windshield Adhesives
- How to Build a Reliable Windshield Adhesive Sample Evaluation
- Define the application and risk profile before testing
- Control samples, substrates, and conditioning
- Use a staged gate instead of a single pass-or-fail trial
- Performance Criteria for Comparing Moisture-Curing PU Bonding Systems
- Evaluate application behavior and production efficiency
- Measure adhesion, elasticity, and failure mode
- Assess environmental resistance and safety-related documentation
- Turning Laboratory Results into a Procurement Decision
- Weight technical performance against total cost
- Verify supplier quality and continuity
- Why KINGDELI is a qualified partner for broader sealant programs
- Frequently Asked Questions
A reliable polyurethane adhesive for windshield evaluation requires more than a cartridge trial or a simple visual inspection. B2B buyers should assess the complete bonding system, including glass, painted metal, ceramic frit, primer, activator, application equipment, curing conditions, storage stability, worker safety, and vehicle release requirements. A controlled sample protocol should measure workability, open time, adhesion, cohesive strength, moisture-curing behavior, temperature resistance, aging performance, and compatibility with production processes. The objective is to confirm that a candidate material can deliver repeatable windshield retention, efficient line handling, regulatory compliance, and predictable total cost across real operating conditions.
How to Build a Reliable Windshield Adhesive Sample Evaluation
Define the application and risk profile before testing
The first step is to document the intended use rather than asking suppliers for a general-purpose sealant. A replacement-glass workshop may prioritize fast drive-away time, low odor, easy nozzle cutting, and adhesion to existing paint. An automotive manufacturer may require robotic dispensing, stable bead geometry, short takt time, resistance to body flex, and documented compatibility with glass encapsulation or primer systems. Commercial vehicle, bus, rail, and specialty vehicle applications can impose different requirements for vibration, thermal cycling, weathering, and repairability.
The specification should identify glass type, ceramic frit, coating, encapsulation material, body substrate, paint system, primer, activator, bead dimensions, target cure time, storage temperature, and expected service environment. Buyers should also establish whether the adhesive is part of a safety-critical glazing assembly. In that case, the supplier must explain how product performance relates to applicable vehicle and glazing requirements, such as FMVSS 212 for windshield mounting in the United States and relevant regional regulations.
Control samples, substrates, and conditioning
Comparison is meaningful only when every supplier receives equivalent test conditions. Use production-representative glass panels, body paint coupons, ceramic frit, primers, and surface cleaners. Record the substrate manufacturer, batch number, surface energy if available, cleaning method, elapsed time between preparation and application, and ambient temperature and humidity. A sample that performs well on laboratory glass but fails on a low-energy coating or aged paint system creates avoidable launch risk.
Prepare at least three categories of specimens: fresh untreated substrates, production-prepared substrates, and deliberately challenging substrates such as low-temperature glass or aged painted panels. Store materials according to the supplier’s technical data sheet and record cartridge age, lot number, packaging condition, and temperature history. Moisture-curing products are particularly sensitive to storage and environmental exposure, so a buyer should never combine opened and unopened packaging in one test group.
Use a staged gate instead of a single pass-or-fail trial
A practical protocol uses four gates. Gate one screens packaging, extrusion, appearance, odor, and basic adhesion. Gate two measures application behavior and early strength. Gate three examines accelerated durability and failure mode. Gate four confirms line integration, documentation, and commercial supply readiness. This sequence prevents expensive environmental testing on a material that already has unacceptable dispensing or substrate-compatibility problems.
Each result should be recorded numerically wherever possible. Useful fields include bead mass per meter, extrusion pressure, skin formation time, tack-free time, cure depth after 24 and 48 hours, lap-shear or peel strength, percentage cohesive failure, dimensional change, and drive-away or handling time. A photographic record of bead shape and fracture surfaces adds valuable evidence, but photographs should support—not replace—instrumented measurements.
Performance Criteria for Comparing Moisture-Curing PU Bonding Systems
Evaluate application behavior and production efficiency
Operators should test the adhesive with the dispensing method used in production: manual sausage gun, pneumatic gun, battery applicator, or automated pump. Measure extrusion force at the lowest and highest expected temperatures. Excessive force increases operator fatigue and can cause inconsistent bead placement, while overly soft material may slump, string, or produce an irregular profile. A stable bead should maintain its designed width and height during the time between application and glass placement.
Open time must be evaluated under realistic humidity and temperature conditions. Buyers should record the interval from primer or adhesive application to glass installation, then inspect whether the surface has skinned, transferred, or lost wetting capability. The test should include the fastest and slowest takt times expected on the production line. A product that performs only within a narrow time window can generate rework when staffing, climate, or vehicle sequencing changes.
Early strength is important for vehicle movement, but it should not be judged by cure speed alone. The evaluation should confirm that rapid handling does not compromise wetting, interfacial adhesion, or long-term elasticity. For a safety-related glass bond, a supplier should explain the basis for its stated safe drive-away time and identify the temperature and humidity conditions supporting that claim.
Measure adhesion, elasticity, and failure mode
Adhesion testing should cover every relevant interface: adhesive to glass, adhesive to ceramic frit, adhesive to primer, adhesive to painted steel, and adhesive to any approved encapsulation. A useful result is not merely the highest force value. The inspection must determine whether failure is adhesive at the interface or cohesive within the cured polymer. Predominantly cohesive failure generally indicates that the interface is stronger than the adhesive body, although acceptance criteria must be defined for the specific design and standard.
Peel, tensile, lap-shear, and bead-pull methods can reveal different weaknesses. The ASTM C794 peel adhesion method is commonly associated with elastomeric joint sealants and can help compare prepared interfaces when the method is suitable for the formulation. Movement capability and durability should also be considered with reference to recognized sealant classification principles such as ISO 11600. These references do not automatically certify an automotive glazing adhesive; they help buyers structure a technically defensible test plan.
Elastic recovery matters because a windshield assembly experiences body flex, vibration, temperature changes, and differential movement between glass and metal. Measure hardness, tensile behavior, elongation, and modulus after curing, then repeat selected tests after heat, humidity, water immersion, and thermal cycling. The best candidate balances sufficient green strength with a flexible cured network that does not become brittle or detach from the substrate.
Assess environmental resistance and safety-related documentation
Accelerated aging should represent the vehicle’s expected environment rather than rely on one generic oven exposure. Useful conditions include hot-humid aging, freeze-thaw cycles, ultraviolet exposure where relevant, salt contamination, water immersion, and temperature cycling. After conditioning, inspect bond continuity, edge lifting, cracking, bubbles, discoloration, hardness change, and fracture mode. Testing should compare aged specimens with unaged controls and define an acceptance threshold before the results are available.
Buyers should request the safety data sheet, technical data sheet, certificate of analysis, shelf-life statement, storage requirements, and change-control policy. Review volatile organic compound information, isocyanate communication, workplace ventilation guidance, personal protective equipment requirements, and waste-handling instructions. Product stewardship should align with the buyer’s regional obligations; ISO 14001 can provide a useful framework for evaluating a supplier’s environmental management system, while ISO 9001 supports review of quality-management controls.
| Evaluation area | Recommended observation | Buyer decision signal |
|---|---|---|
| Extrusion and dispensing | Force, bead uniformity, stringing, sag, and equipment compatibility at operating temperatures | Stable application without excessive operator or equipment load |
| Open time | Skin formation, wetting, transfer, and installation window under low and high humidity | Consistent placement across the planned takt-time range |
| Initial cure | Handling strength, cure depth, and safe movement time at specified conditions | Documented release criteria supported by test evidence |
| Interface adhesion | Glass, frit, primer, paint, and encapsulation adhesion with fracture-mode analysis | Repeatable bonding with acceptable cohesive-failure results |
| Durability | Thermal cycling, humidity, water, UV where relevant, and post-aging inspection | No unacceptable cracking, lifting, embrittlement, or interfacial failure |
| Supply qualification | Lot consistency, shelf life, packaging, traceability, technical support, and change notification | Low interruption risk throughout the vehicle program |
Turning Laboratory Results into a Procurement Decision
Weight technical performance against total cost
Unit price is only one part of the economic evaluation. Buyers should calculate material consumption per vehicle, primer and activator usage, waste from nozzle changes, labor time, equipment cleaning, rework, rejected glass, inventory carrying cost, and production downtime. A lower-priced cartridge may become more expensive if it requires a wider bead, creates more waste, has a short shelf life, or generates installation delays.
Build a weighted scorecard before commercial negotiations. A representative model may assign high importance to adhesion and durability, followed by early strength, process window, application ergonomics, documentation, supply continuity, and price. The weighting should reflect the cost of failure. For a safety-critical glazing program, a small price advantage should not outweigh uncertain field performance or weak change-control practices.
Verify supplier quality and continuity
Supplier qualification should include manufacturing-site capability, raw-material controls, batch release testing, retained samples, complaint handling, and corrective-action procedures. Ask how the manufacturer manages formulation changes, alternate raw materials, packaging changes, and production transfers. Buyers should also confirm minimum order quantities, lead times, regional inventory, export documentation, and the ability to support demand increases.
Quality-system certification is useful, but a certificate alone does not prove product suitability. Request formulation-specific test reports, lot-to-lot data, application guidance, and references for comparable substrates or vehicle programs where disclosure is permitted. A robust supplier will distinguish validated claims from recommended starting conditions and will identify which variables must be confirmed by the customer.
Why KINGDELI is a qualified partner for broader sealant programs
Our team at KINGDELI supports buyers that require both a windshield bonding material and a broader sealants and adhesives supply strategy. Established in 1998 and headquartered in Foshan, China, KINGDELI operates a 66,000 m² facility with fully automated production lines and annual capacity exceeding 100,000 tons. This scale supports consistent supply, structured batch control, and planning support for distributors, vehicle-related manufacturers, construction partners, and industrial buyers.
We combine manufacturing capability with technical development across Polyurethane Sealant, MS polymer Sealant, neutral silicone sealant, acetic silicone sealant, Acrylic Sealant, and silicone glazing sealant. This portfolio allows procurement teams to consolidate compatible products where appropriate while maintaining application-specific specifications. No More Nails adhesive, RTV Gasket Maker, Epoxy Tile Grout, and Self-Leveling Sealant extend the range for assembly, maintenance, glazing, repair, and construction applications.
As a recognized National High-Tech Enterprise and a contributor to National Standard GB/T 29755-2013, we place emphasis on documented performance and process discipline. Our management systems and product development work support international business requirements, including ISO 9001, ISO 14001, CE, and ASTM-related expectations where applicable to the product and market. Certification and test relevance should always be confirmed against the exact formulation, application, and destination market.
With more than 27 years of industry expertise and customers in over 50 countries, we provide OEM and ODM support, low-VOC formulation options, packaging customization, and technical service. Our engineering team can help structure sample comparisons around substrate preparation, bead design, curing conditions, and production equipment rather than treating the cartridge as an isolated commodity. This approach helps buyers reduce qualification uncertainty and establish a practical path from laboratory screening to controlled field validation.
For a final approval, the buyer and supplier should sign off on the approved substrate list, application sequence, primer system, bead dimensions, environmental limits, cure and release criteria, packaging, lot traceability, and change-notification requirements. The result should be a controlled product specification and process instruction—not merely a favorable sample report.
Frequently Asked Questions
What should B2B buyers test first when evaluating a windshield bonding adhesive?
Buyers should first screen packaging, extrusion, appearance, odor, basic adhesion, substrate compatibility, and storage condition before moving to accelerated durability testing.
Which substrates should be included in a windshield adhesive evaluation?
Testing should include production-representative glass, ceramic frit, painted metal, approved primers, surface cleaners, coatings, and any relevant encapsulation materials, along with challenging aged or low-energy surfaces.
How should buyers evaluate the open time of a PU glazing adhesive?
Record the interval from primer or adhesive application to glass installation and inspect skin formation, transfer, wetting, and bond quality under the fastest and slowest expected production takt times and relevant humidity conditions.
Why is cohesive failure important in adhesive testing?
Cohesive failure indicates that fracture occurs within the cured adhesive rather than at the interface, helping show that the prepared substrate bond is stronger than the adhesive body; acceptance criteria must still be defined for the specific application.
What documents should a supplier provide during qualification?
A supplier should provide a safety data sheet, technical data sheet, certificate of analysis, shelf-life and storage information, application instructions, test reports, quality certifications, and a change-control policy.
How can buyers compare the total cost of windshield adhesives?
The comparison should include unit price, material consumption, primer and activator usage, waste, labor, equipment cleaning, rework, rejected glass, inventory costs, shelf life, and potential production downtime.
What does KINGDELI provide beyond polyurethane windshield bonding products?
KINGDELI provides polyurethane, MS polymer, neutral and acetic silicone, acrylic, silicone glazing, No More Nails, RTV Gasket Maker, Epoxy Tile Grout, and Self-Leveling Sealant products, together with OEM/ODM support, low-VOC options, manufacturing scale, and technical service.
Avoid These 7 Common MS Sealant Mistakes: The Secret to Long-Lasting, Leak-Proof Joints
OEM/ODM acetic cure silicone sealant Manufacturers and Suppliers
Construction Sealant Samples: What to Test Before a Bulk Purchase
Quality Tests for Silicone Sealant for Windows and Doors Suppliers
HY992 Modified Polyurethane Construction Sealant
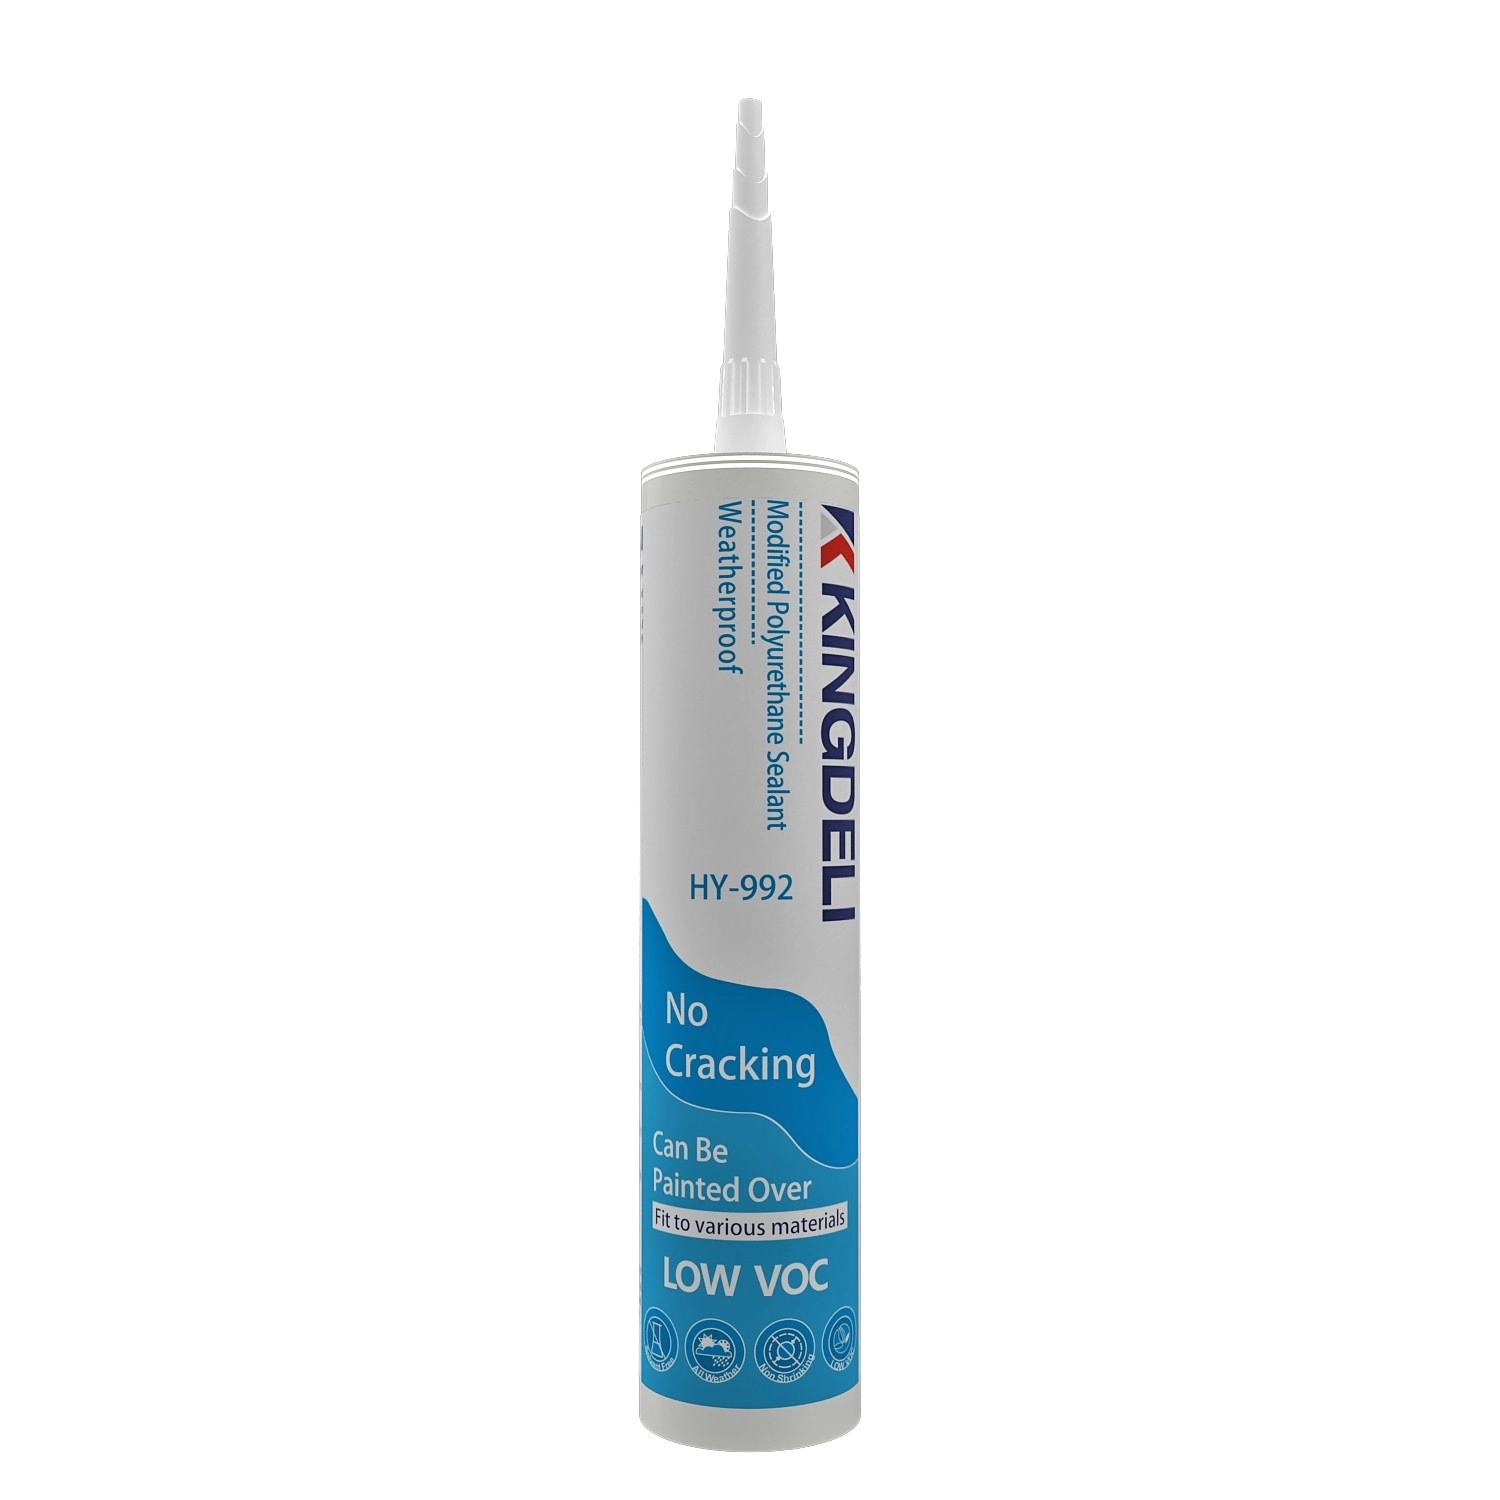
HY992 Modified Polyurethane Sealant is a one-component, moisture-curing construction sealant designed for professional building and structural sealing applications. It provides excellent adhesion, weather resistance, and durable elasticity, making it suitable for a wide range of construction materials.
The formulation delivers strong bonding performance without corrosion or substrate contamination, while maintaining low VOC content for environmentally responsible construction projects.

HY995 Crystal Clear Ms Polymer Adhesive/Sealant
HY995 Crystal Clear Ms Polymer Adhesive/Sealant is a new generation MS Polymer adhesive / sealant formulated for all bonding and sealing applications where long term reliability is required. It has excellent bonding strength on various materials. It will cure to form a durable, flexible, waterproof seal.

HY997 High-Performance Anti-Microbial MS Polymer Sealant
HY997 MS polymer sealant for is is a premium one-component, neutral-curing modified silane sealant engineered for demanding interior applications. It offers a Class 20 movement capability, ensuring long-lasting flexibility and reliable performance under dynamic joint conditions. Curing at room temperature, HY997 delivers superior anti-microbial and mildew-resistant properties, maintaining hygienic and clean environments over time.
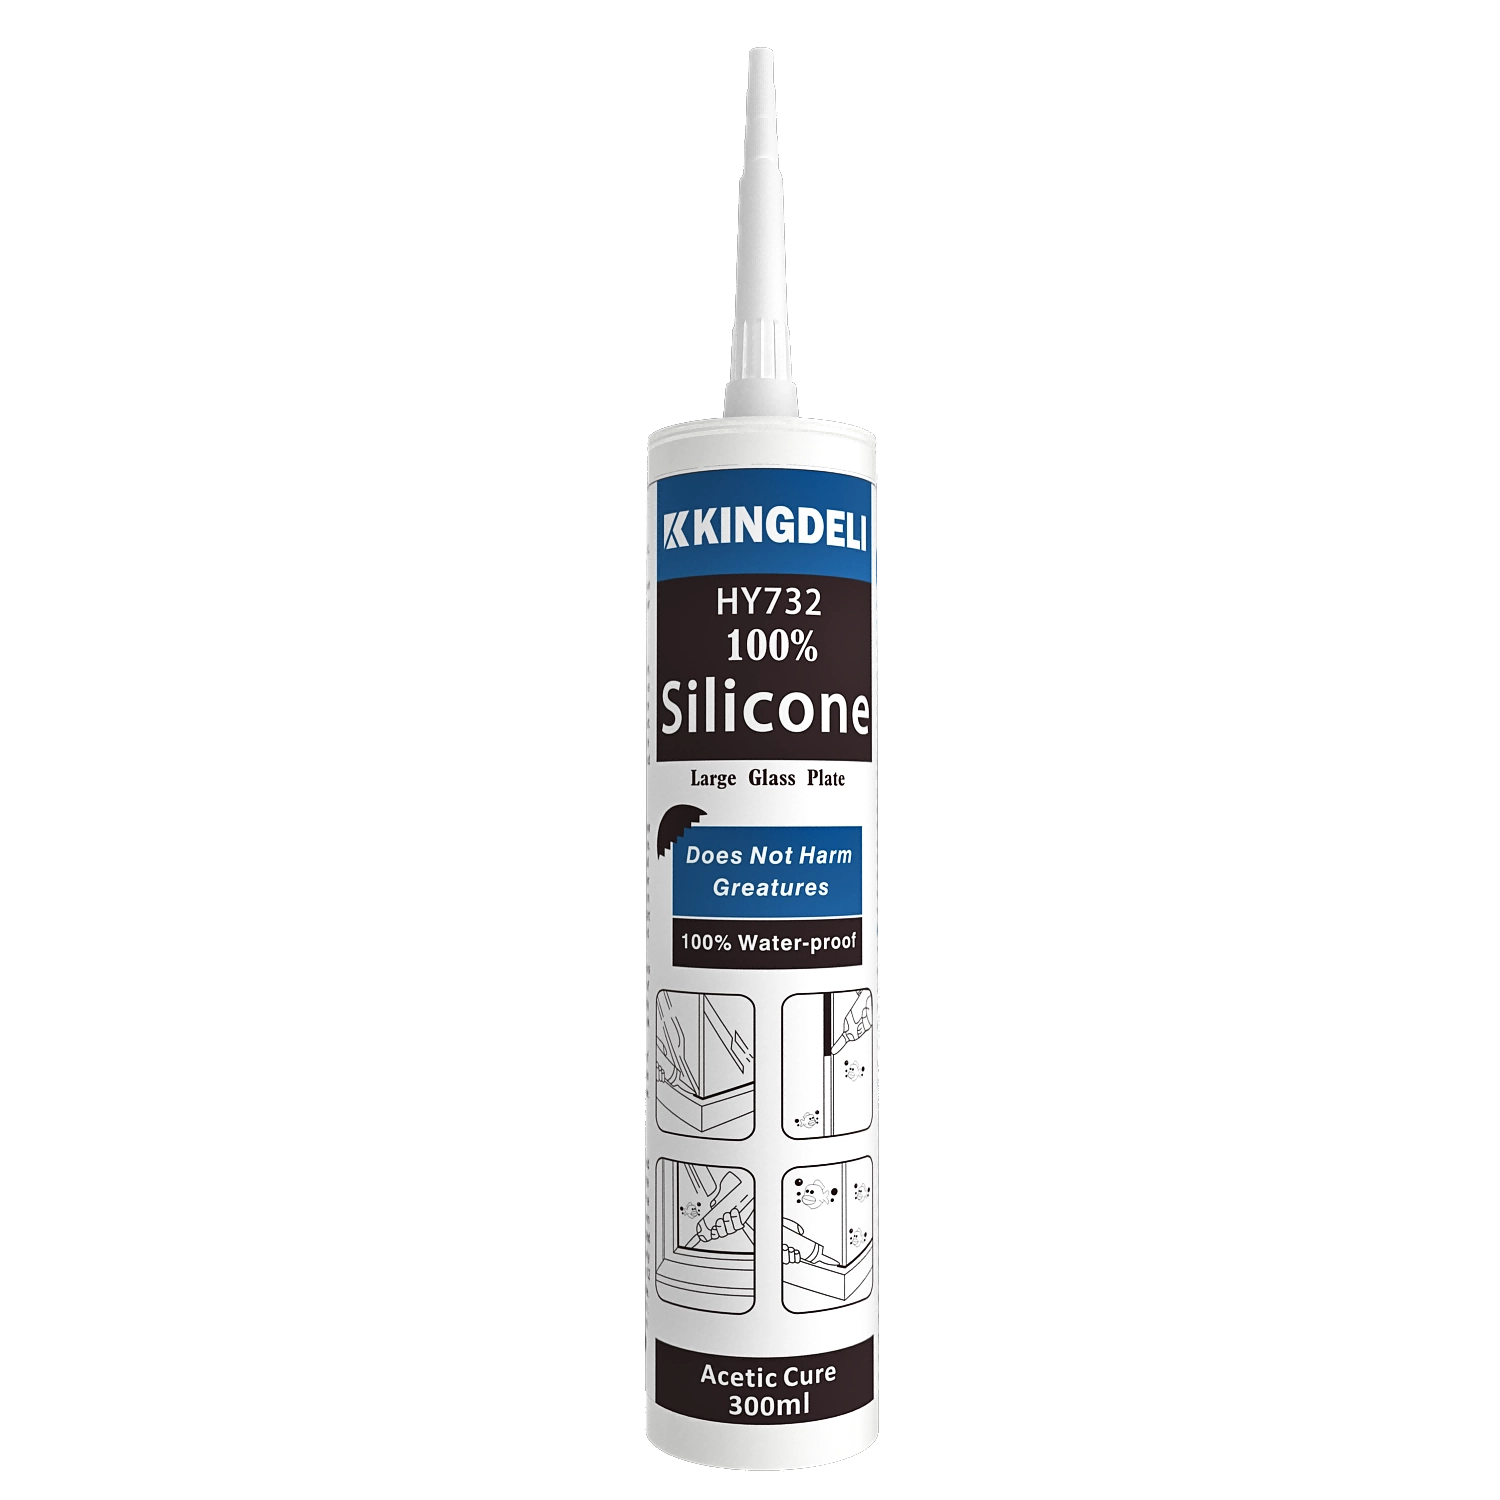
KINGDELI HY732 Professional Acetoxy Cure Silicone Sealant
KINGDELI HY732 is a professional-grade, one-component acetoxy cure silicone sealant designed for fast curing, strong adhesion, and long-lasting flexibility. Ideal for aquariums, glass applications, aluminum doors and windows, kitchens, and bathrooms, it provides reliable sealing performance with excellent anti-fungal protection in high-humidity environments.
Let’s Build Stronger Bonds with Quality Adhesives and Sealants
Have questions about the topic or need tailored sealant solutions for your project?
Our team is ready to provide expert guidance, product recommendations, and application support.
Innovating with Integrity, Bonding the World
Since 1998, KINGDELI has delivered trusted, sustainable sealant solutions that connect industries and inspire progress worldwide.
Whatsapp: +8618825946249
Kingdeli
Kingdeli
Kingdeli
Kingdeli
Kingdeli