Case Study: Cost Savings Switching PU Adhesive Suppliers at Scale
- How a High-Volume Automotive Bonding Program Identified Hidden Cost
- The procurement problem behind the supplier change
- Why the lowest unit price was not the lowest total cost
- The baseline measurement system
- The Supplier-Switch Method That Protected Quality and Continuity
- Technical qualification before commercial negotiation
- Controlled line trials and operator adoption
- Commercial controls beyond the purchase order
- Financial Results: Measuring Total Applied Cost at Scale
- The cost model used by the project team
- How quality improvements became measurable savings
- Payback and risk management
- Why KINGDELI Is Positioned for Large-Scale Adhesive Supply
- Manufacturing capacity and supply consistency
- Technical breadth across sealants and adhesives
- Quality systems, compliance, and technical partnership
- A practical buyer checklist for the next sourcing event
- Frequently Asked Questions
A large automotive component manufacturer reduced its annual bonding expenditure after replacing its incumbent supplier of polyurethane adhesive for windshield applications with a qualified high-volume partner. The improvement did not come from purchasing the lowest-priced cartridge. It resulted from a controlled supplier-switching program that measured material consumption, open time, curing behavior, rework, packaging waste, freight, line stoppages, and technical support. For buyers of sealants and adhesives, the case demonstrates that the commercial value of a supplier change depends on total applied cost and validated process performance rather than quoted price per kilogram alone.
How a High-Volume Automotive Bonding Program Identified Hidden Cost
The procurement problem behind the supplier change
The manufacturer operated several production lines and consumed a moisture-curing polyurethane bonding compound for glass installation and related vehicle assembly work. The incumbent material met the basic application requirement, but purchasing records revealed several recurring issues: inconsistent extrusion resistance between batches, variable skin formation, excessive residual material in packs, and occasional curing delays during humid production periods. Each issue appeared small when viewed separately. Together, they increased labor time, material usage, inspection effort, and production risk.
The initial purchasing comparison focused on the supplier’s price per sausage or cartridge. That approach excluded the cost of nozzle replacement, purge material, rejected assemblies, operator waiting time, emergency deliveries, and short-dated inventory. A more complete analysis followed the adhesive from receipt to final vehicle release. This included incoming quality control, storage, conditioning, dispensing, bead placement, glass positioning, fixture time, final inspection, and warranty-related documentation.
Why the lowest unit price was not the lowest total cost
In industrial bonding, a lower price can be offset by a higher consumption rate. A compound that requires a wider bead to achieve the same joint geometry may increase annual usage even when its quoted price is attractive. Likewise, poor wetting or unstable extrusion can create discontinuities that require rework. The buyer therefore needs a cost model based on cost per completed assembly, not simply cost per container.
The evaluation also considered technical risk. Windshield bonding is a safety-relevant process, so a supplier change must not compromise adhesion, primer compatibility, curing, environmental resistance, or the manufacturer’s validated safe-drive-away procedure. Product selection should be aligned with the applicable vehicle and glazing requirements, while regulatory references such as the U.S. Federal Motor Vehicle Safety Standard 212 should be reviewed where relevant to the vehicle program and market.
The baseline measurement system
Before the trial, the project team established a twelve-week baseline. It recorded adhesive consumption per vehicle, average bead length, dispensing pressure, open time, fixture time, first-pass yield, rework frequency, cartridge utilization, line interruptions, and freight cost. Quality personnel also retained samples from multiple production lots to compare viscosity, skin formation, tensile behavior, and cured adhesion under the actual substrate and surface-preparation conditions.
This baseline prevented an unreliable before-and-after comparison. A new supplier can appear successful if the trial occurs during a low-volume period or with unusually favorable weather. Conversely, an excellent formulation can appear weak if operators use an unsuitable nozzle, store the material outside the recommended range, or alter the bead geometry without engineering approval.
The Supplier-Switch Method That Protected Quality and Continuity
Technical qualification before commercial negotiation
The replacement program began with a technical specification rather than a price request. The specification defined substrates, bead dimensions, application temperature, storage limits, packaging format, curing profile, adhesion expectations, appearance requirements, documentation, lot traceability, and escalation procedures. It also identified which parameters were critical to quality and which could be optimized for productivity.
Laboratory screening was followed by production-line validation. The candidate material was evaluated on representative glass, painted metal, coated surfaces, and other approved substrates. Tests covered initial green strength, cohesive failure behavior, elastic recovery, resistance to moisture and temperature cycling, and compatibility with primers or cleaners. Where standard methods were used, the engineering team mapped the test plan to recognized quality systems such as ISO 9001 quality management principles and the customer’s own validation protocol.
Controlled line trials and operator adoption
A controlled trial used the same dispensing equipment, nozzle geometry, bead profile, work instructions, and inspection criteria applied to the incumbent product. Operators were trained on extrusion force, cut-off technique, pack loading, surface preparation, and material conditioning. This was essential because a formulation change may require a minor adjustment in pressure or nozzle selection even when the application remains familiar.
The trial was released in stages. First, a small production batch verified handling and appearance. Second, a larger batch tested shift-to-shift consistency. Third, the candidate supplier supported extended production under normal humidity and temperature variation. Quality gates were established for adhesion, cure, bead continuity, contamination control, and final assembly release. No commercial savings were counted until the candidate material met the agreed technical criteria.
Commercial controls beyond the purchase order
The new supply agreement included a defined product specification, change-notification period, certificate-of-analysis requirements, batch traceability, shelf-life commitments, emergency response expectations, and a forecast-based delivery plan. These controls reduced the risk that a supplier would change raw materials or manufacturing parameters without customer approval.
Packaging was also reviewed. Larger packs reduced packaging waste and changeover frequency, but only where the line could consume the material within its usable period. Smaller packs improved flexibility for lower-volume stations. The preferred format was selected by comparing waste, handling time, storage space, dispensing reliability, and disposal costs. This is a practical example of why procurement, engineering, production, quality, and logistics should jointly approve an adhesive supplier.
| Cost or performance measure | Incumbent baseline | Validated replacement | Illustrative annual effect |
|---|---|---|---|
| Material consumption per assembly | 100% baseline | 94% | 6% lower usage |
| Purchase price per kilogram | 100% baseline | 96% | 4% lower quoted price |
| First-pass yield | 98.4% | 99.2% | Fewer rework events |
| Packaging residual waste | 100% baseline | 70% | 30% lower residual waste |
| Line interruptions attributed to adhesive handling | 18 events per year | 7 events per year | 11 fewer interruptions |
| Freight and expedited delivery cost | 100% baseline | 82% | 18% lower logistics cost |
The figures in this table are an illustrative case model showing how a buyer can structure a business case; they are not presented as a universal industry benchmark. In practice, the financial result depends on annual volume, bead dimensions, labor rates, line speed, packaging, freight distance, local taxes, and the cost assigned to downtime. The calculation should therefore be rebuilt using the buyer’s verified production records.
Financial Results: Measuring Total Applied Cost at Scale
The cost model used by the project team
The business case combined five cost categories: adhesive purchase, consumption variance, direct labor, quality losses, and supply-chain overhead. The formula was simple: total annual adhesive cost equals purchased material plus application waste, rework, downtime, freight High Qualitys, and disposal. The replacement supplier was approved only after the model showed a positive return under conservative assumptions.
At the plant level, the reduction in material consumption produced the largest recurring benefit. More stable extrusion helped operators maintain the specified bead size instead of compensating with excess material. Better pack utilization reduced the amount left inside containers at changeover. Improved lot consistency also reduced the need for repeated line adjustments. These gains were modest per vehicle but significant across a high-volume program.
How quality improvements became measurable savings
Quality savings were calculated from actual rework records rather than estimated percentages. Each reworked assembly was assigned a material cost, labor cost, inspection cost, and production delay. The analysis excluded any benefit that could not be demonstrated through traceable records. This protected the project from overstating its return and gave finance a defensible basis for approval.
Warranty exposure was treated separately from routine rework. A bonding failure may create costs long after production, including vehicle recovery, replacement glass, field labor, customer support, and reputation damage. A supplier’s technical documentation, batch traceability, and change-control discipline therefore have economic value even when they do not appear on the purchase invoice. Buyers should also distinguish between a supplier’s product certificate and evidence that the material has been validated on the specific substrates and process used by the manufacturer.
Payback and risk management
The project achieved payback through a combination of lower consumption, fewer interruptions, improved pack utilization, and reduced expedited freight. However, the team retained dual-source or contingency stock during the initial ramp-up. A low-cost supplier switch is not successful if it creates a single point of failure or causes production to stop while technical issues are investigated.
A robust implementation plan includes safety stock, a documented rollback procedure, parallel quality approval, operator training, and scheduled performance reviews at thirty, sixty, and ninety days. Key indicators should include incoming lot acceptance, bead consistency, curing time, first-pass yield, complaints, delivery performance, and cost per completed assembly.
Why KINGDELI Is Positioned for Large-Scale Adhesive Supply
Manufacturing capacity and supply consistency
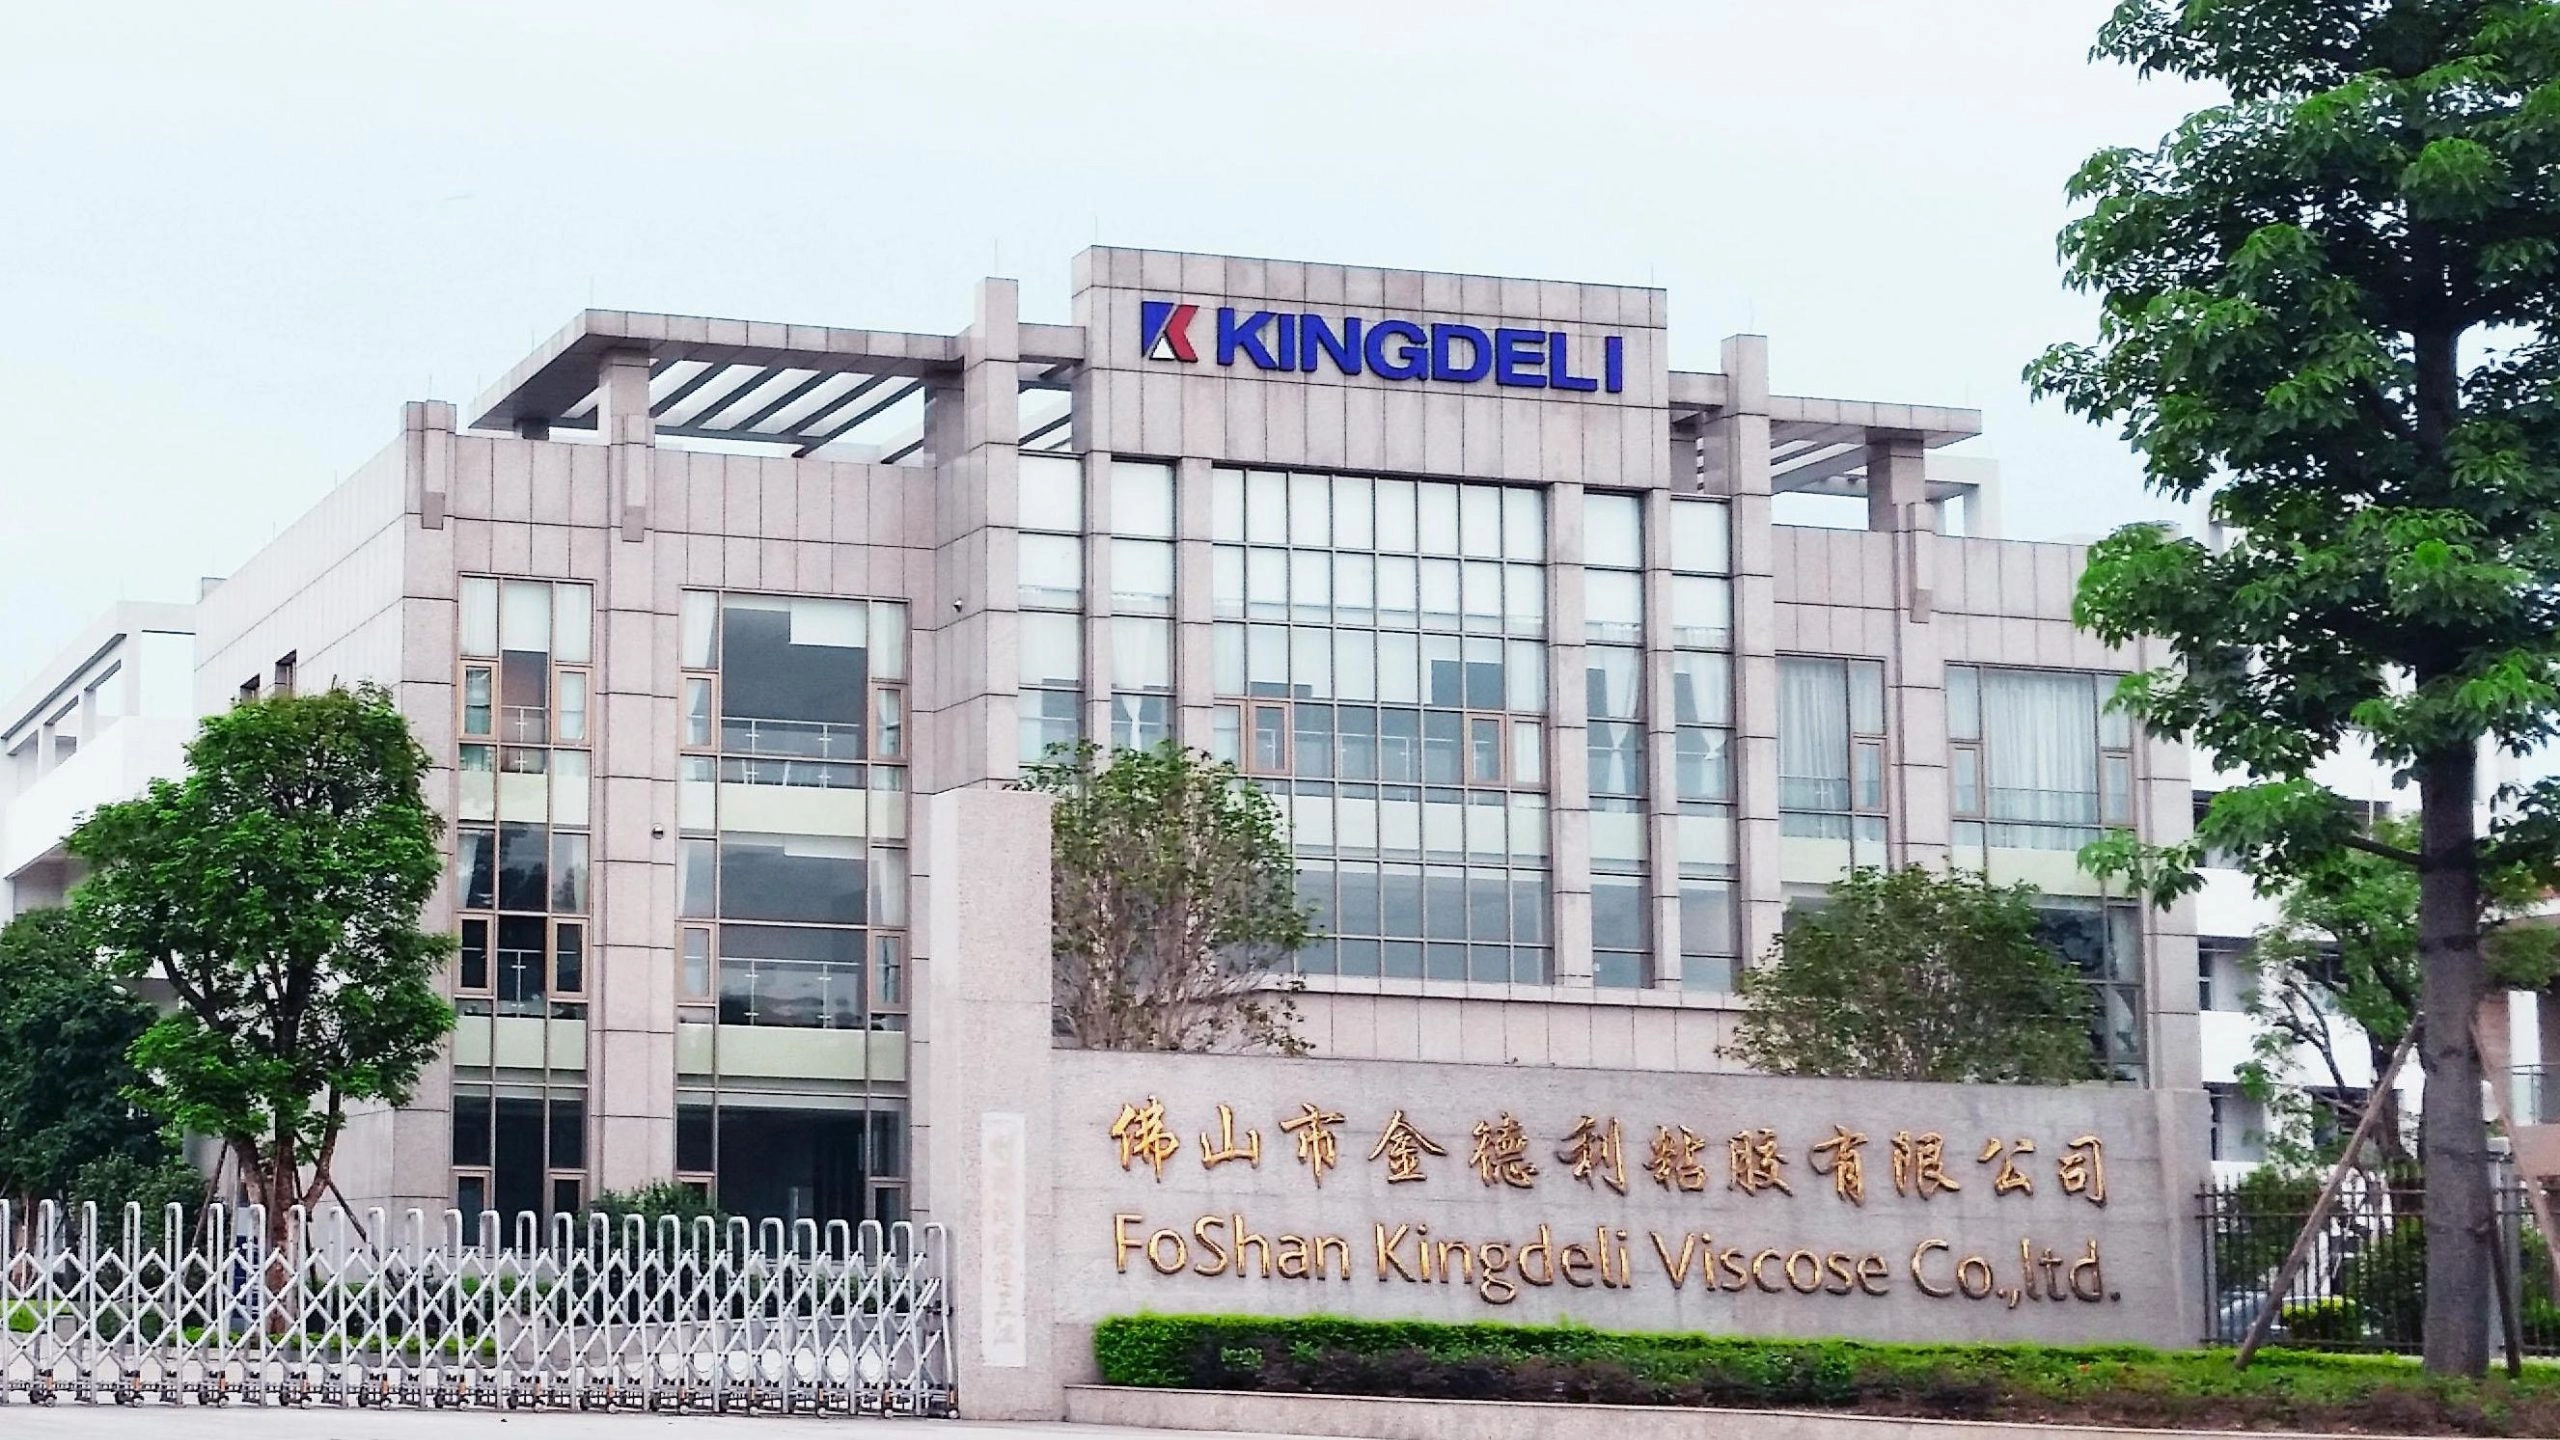
We established KINGDELI in 1998 and have developed the company into a global manufacturer of high-performance sealants, adhesives, and coatings. Our headquarters and 66,000 m² production facility are located in Foshan, China. Fully automated production lines support annual capacity exceeding 100,000 tons, giving distributors, automotive suppliers, construction manufacturers, and industrial operators a stronger foundation for planned volume programs.
Large-scale buyers need more than a technically acceptable formulation. They need repeatable batches, stable packaging, predictable lead times, production records, and responsive escalation. Our manufacturing system is designed to support those requirements while allowing customers to define packaging, branding, application requirements, and delivery schedules through OEM and ODM cooperation.
Technical breadth across sealants and adhesives
Our product portfolio includes neutral silicone sealant, acetic silicone sealant, acrylic sealant, silicone glazing sealant, polyurethane sealant, MS polymer sealant, No More Nails adhesive, RTV gasket maker, epoxy tile grout, and self-leveling sealant. This range allows procurement teams to consolidate selected categories without forcing one chemistry into applications where another technology is more appropriate.
For automotive and industrial bonding programs, our engineering approach considers substrate preparation, joint movement, cure conditions, dispensing equipment, packaging, and required documentation. A polyurethane formulation may be evaluated for elastic bonding and moisture-curing behavior, while MS polymer products can be considered where low odor, weatherability, or primer-free processing is important. Silicone technologies remain relevant for glazing, weather sealing, and high-temperature or flexible applications. The correct choice depends on the complete assembly specification.
Quality systems, compliance, and technical partnership
KINGDELI is recognized as a National High-Tech Enterprise and has contributed to the development of China’s national standard GB/T 29755-2013. Our management and product systems are supported by ISO 9001, ISO 14001, CE, and ASTM-related requirements where applicable to the product and destination market. Buyers should confirm the exact certificate scope, test method, and product designation during qualification rather than treating a general company certificate as approval for every application.
With more than 27 years of industry expertise and customers in over 50 countries, we support international procurement through technical service, formulation development, documentation, and sustainable low-VOC options. Environmental management is increasingly relevant to corporate purchasing and facility compliance; the ISO 14001 environmental management framework provides a recognized reference for evaluating systematic environmental practices.
Our supplier-switching support is structured around the buyer’s risk profile. The process can include specification review, sample preparation, laboratory testing, production-line trials, packaging optimization, quality documentation, operator guidance, and post-launch monitoring. This approach helps customers compare a material on performance and total cost while protecting production continuity.
A practical buyer checklist for the next sourcing event
- Define the approved substrates, joint geometry, application temperature, cure requirement, and environmental exposure.
- Request batch traceability, shelf-life data, storage guidance, safety documentation, and change-notification procedures.
- Compare cost per completed assembly, including waste, freight, labor, downtime, and rework.
- Run a controlled production trial using the actual equipment and work instructions.
- Measure first-pass yield, bead consistency, cure behavior, pack utilization, and operator feedback.
- Agree on forecast, safety stock, lead time, corrective-action response, and escalation contacts.
- Review certificates and test reports against the specific product, market, and application rather than relying on generic claims.
The central lesson is that a supplier transition should be treated as an engineered productivity project. When technical validation, procurement analysis, and operational controls are combined, buyers can capture measurable savings without trading away bond reliability or supply resilience. When the decision is based only on unit price, the apparent saving may disappear through excess consumption, quality losses, downtime, or emergency logistics.
Frequently Asked Questions
How should buyers compare polyurethane adhesive suppliers?
Buyers should compare total applied cost rather than price per cartridge or kilogram. The evaluation should include material consumption, packaging waste, labor, rework, downtime, freight, shelf life, technical support, and quality documentation.
What should be validated before changing an automotive bonding adhesive supplier?
The replacement material should be tested on the actual substrates and production equipment. Validation should cover bead consistency, extrusion behavior, open time, curing profile, adhesion, environmental resistance, primer or cleaner compatibility, packaging, and final assembly requirements.
Can a lower-priced adhesive increase total manufacturing cost?
Yes. A lower quoted price can be offset by excessive bead size, residual material in packaging, rework, curing delays, line interruptions, expedited freight, or warranty exposure. The correct metric is cost per completed assembly.
How can a supplier switch avoid production disruption?
The project should use staged line trials, operator training, safety stock, batch traceability, defined change control, a rollback procedure, and performance reviews after launch. Dual-source or contingency inventory may be appropriate during the ramp-up period.
What documents should an industrial adhesive supplier provide?
A qualified supplier should provide product specifications, safety data, shelf-life and storage information, batch traceability, certificates of analysis where applicable, test reports, change-notification procedures, and technical application guidance. Certificate scope should be checked against the exact product and market.
What advantages does KINGDELI offer for high-volume adhesive procurement?
KINGDELI offers a 66,000 m² facility, automated production lines, annual capacity exceeding 100,000 tons, OEM and ODM support, technical service, low-VOC formulation options, and a portfolio covering polyurethane, silicone, MS polymer, acrylic, epoxy, and related adhesive technologies. The company has more than 27 years of industry expertise and serves customers in over 50 countries.
How to Choose the Right MS Sealant for Construction: A Professional Contractor's Checklist for 2026
MS Silicone Sealant for Automotive Assembly and Bonding
OEM/ODM acrylic sealant Manufacturers and Suppliers
High-Temperature Neutral Silicone Sealants for Industry
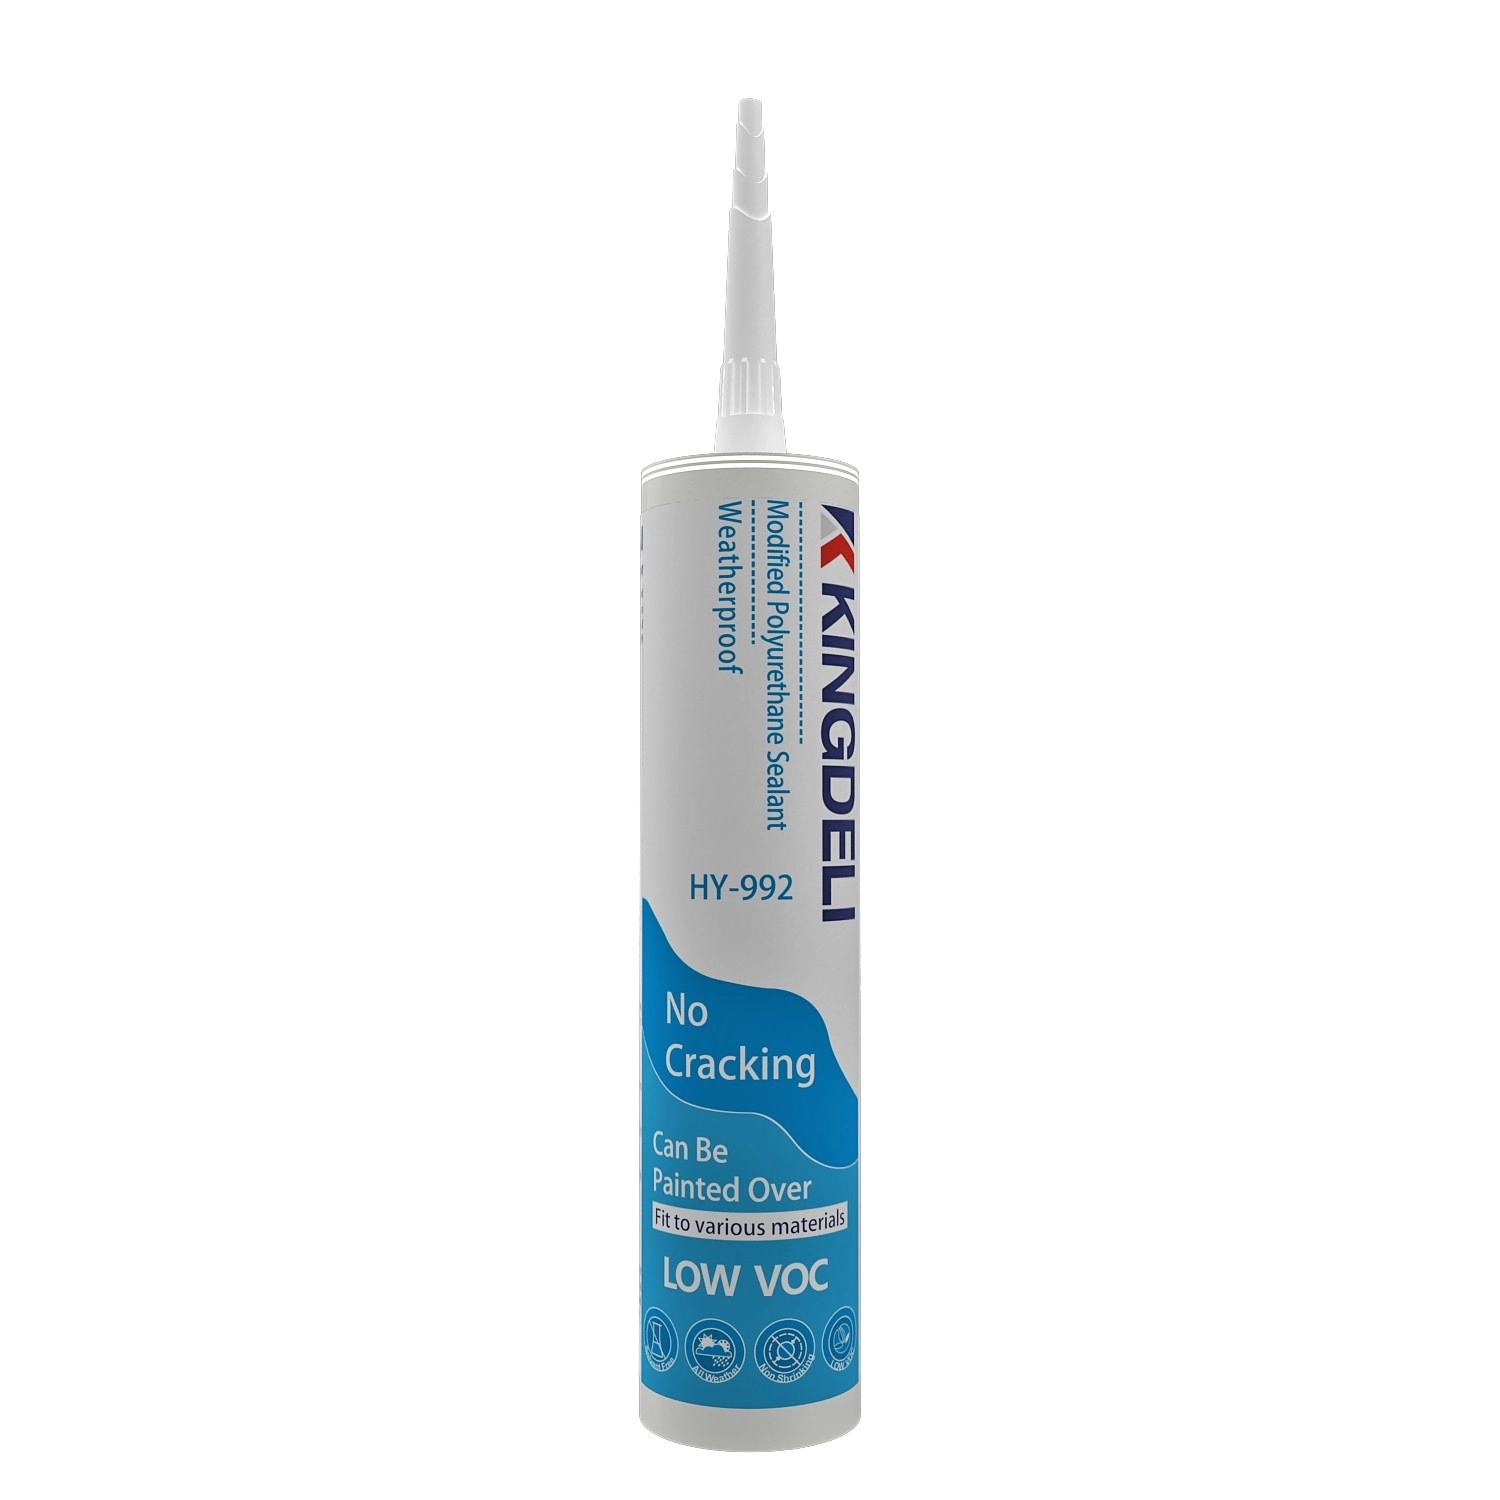
HY992 Modified Polyurethane Construction Sealant
HY992 Modified Polyurethane Sealant is a one-component, moisture-curing construction sealant designed for professional building and structural sealing applications. It provides excellent adhesion, weather resistance, and durable elasticity, making it suitable for a wide range of construction materials.
The formulation delivers strong bonding performance without corrosion or substrate contamination, while maintaining low VOC content for environmentally responsible construction projects.

HY995 Crystal Clear Ms Polymer Adhesive/Sealant
HY995 Crystal Clear Ms Polymer Adhesive/Sealant is a new generation MS Polymer adhesive / sealant formulated for all bonding and sealing applications where long term reliability is required. It has excellent bonding strength on various materials. It will cure to form a durable, flexible, waterproof seal.

HY997 High-Performance Anti-Microbial MS Polymer Sealant
HY997 MS polymer sealant for is is a premium one-component, neutral-curing modified silane sealant engineered for demanding interior applications. It offers a Class 20 movement capability, ensuring long-lasting flexibility and reliable performance under dynamic joint conditions. Curing at room temperature, HY997 delivers superior anti-microbial and mildew-resistant properties, maintaining hygienic and clean environments over time.
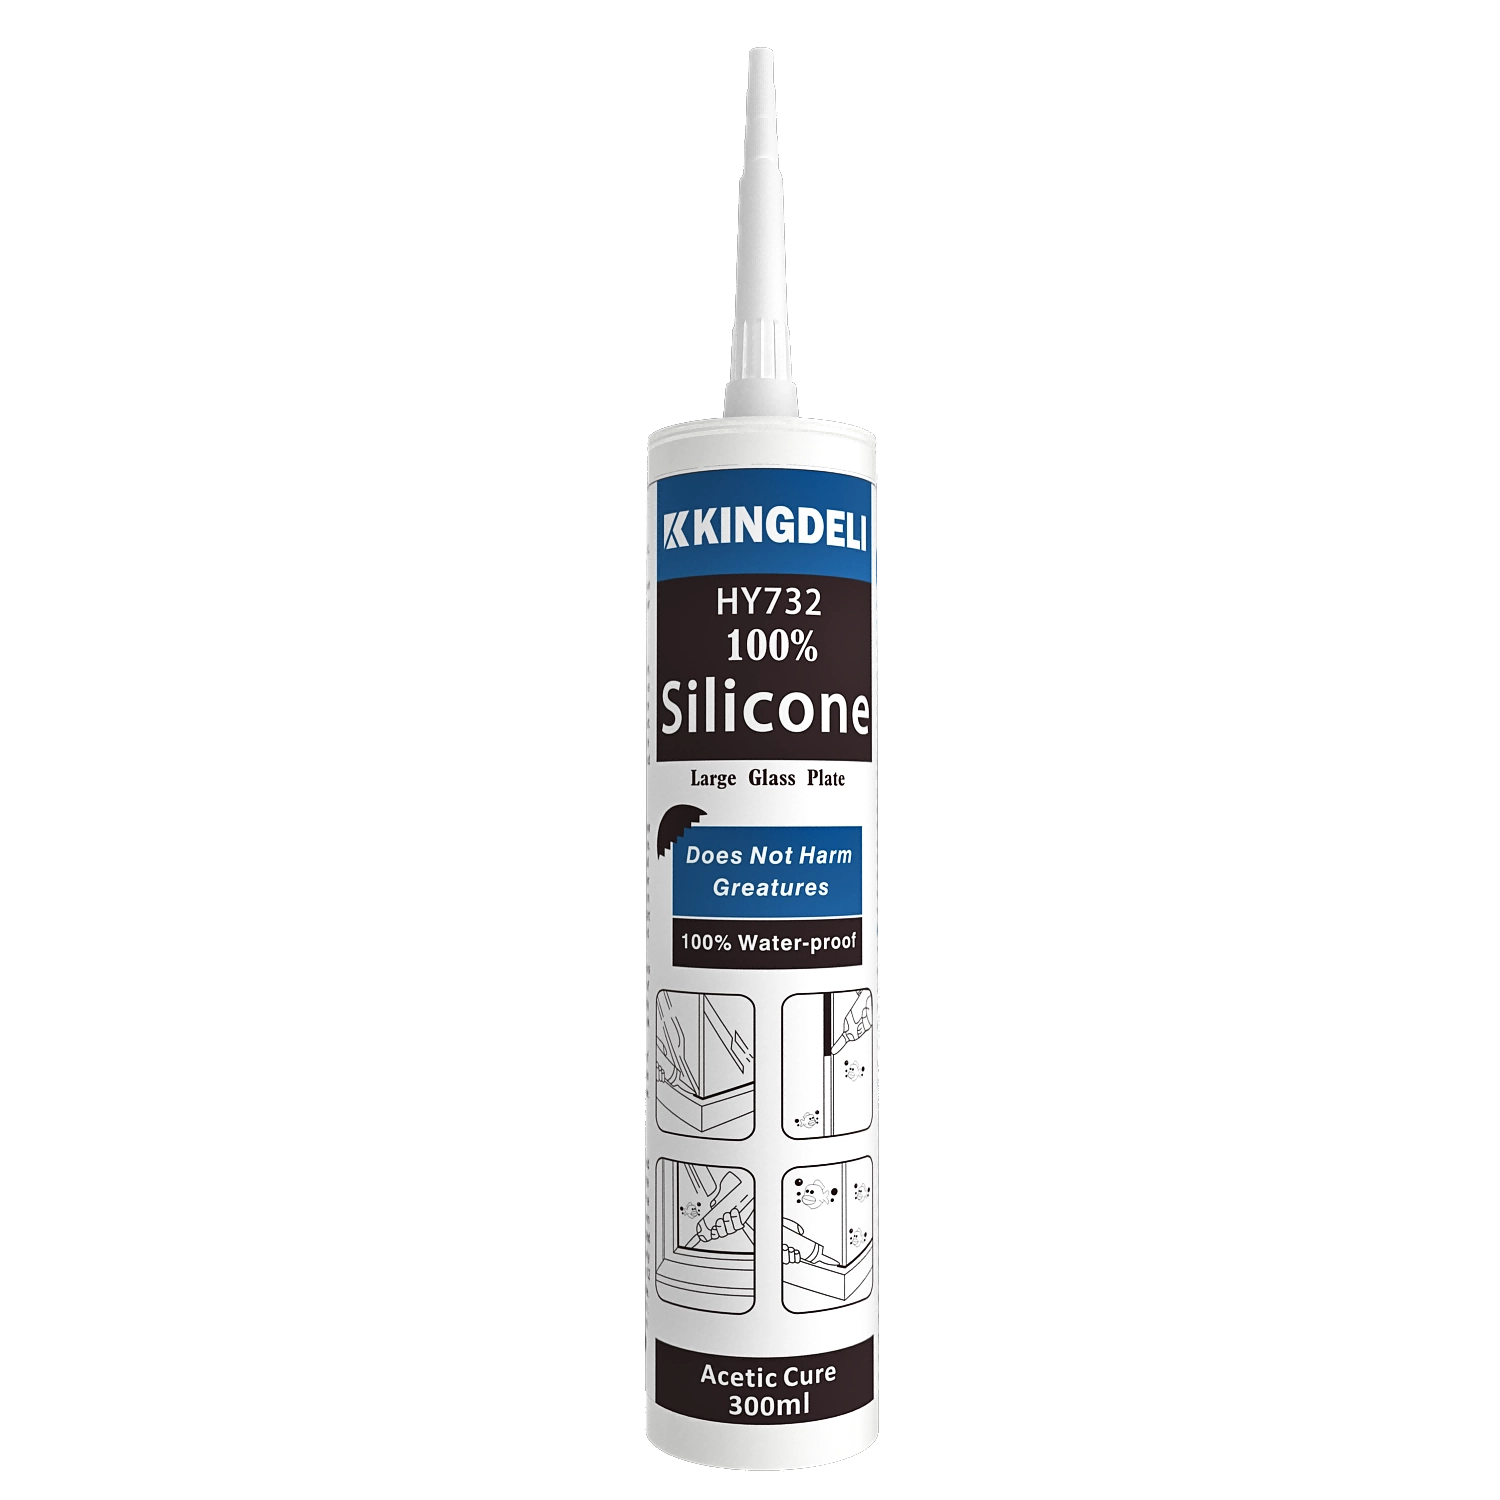
KINGDELI HY732 Professional Acetoxy Cure Silicone Sealant
KINGDELI HY732 is a professional-grade, one-component acetoxy cure silicone sealant designed for fast curing, strong adhesion, and long-lasting flexibility. Ideal for aquariums, glass applications, aluminum doors and windows, kitchens, and bathrooms, it provides reliable sealing performance with excellent anti-fungal protection in high-humidity environments.
Let’s Build Stronger Bonds with Quality Adhesives and Sealants
Have questions about the topic or need tailored sealant solutions for your project?
Our team is ready to provide expert guidance, product recommendations, and application support.
Innovating with Integrity, Bonding the World
Since 1998, KINGDELI has delivered trusted, sustainable sealant solutions that connect industries and inspire progress worldwide.
Whatsapp: +8618825946249
Kingdeli
Kingdeli
Kingdeli
Kingdeli
Kingdeli